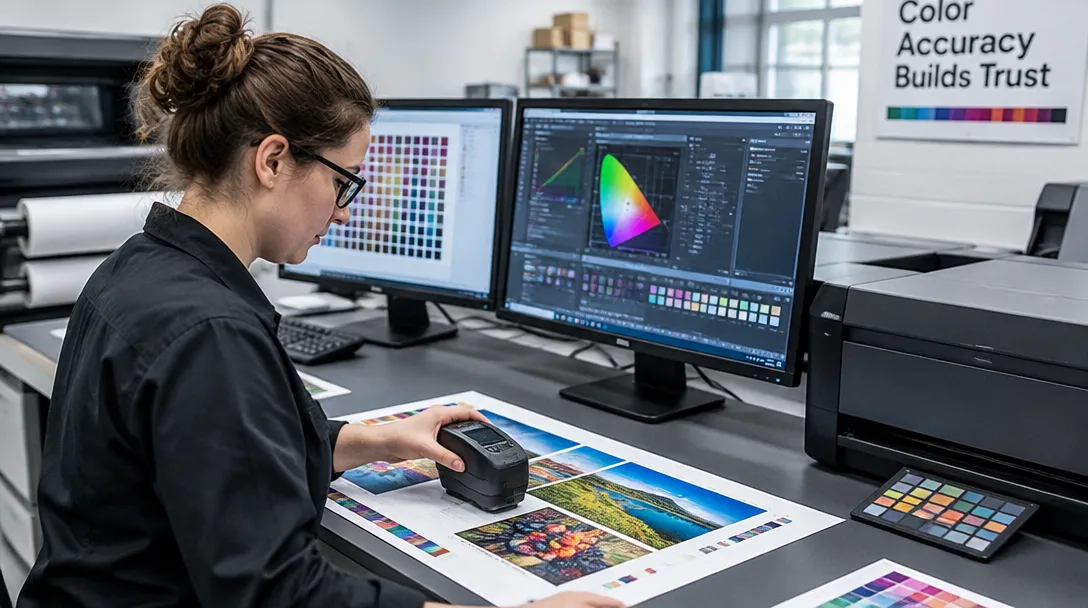
The 10th Fogra Colour Management Symposium gathered over 200 experts from 23 countries and 126 companies in Munich on 25–26 February 2026, with seven sessions covering colour management in packaging printing, proofing on real substrates, HDR in print production, and AI in production workflows. For packaging buyers, the actionable output is clear: specify spatially resolved print evaluation, adopt the FFI ordering standard for ECG 7C, and contractually define proofing substrates and ink-saving digital printing parameters before tooling release.
- The 10th Fogra CMS symposium marked its tenth anniversary with packaging-specific tracks on image-based measurement and spatially resolved print evaluation — a direct upgrade path from spot-density spot checks.
- An FFI ordering standard for ECG 7C (extended colour gamut), derived from a Fogra research report, gives procurement a formal basis to write 7-colour process specs into RFQs.
- Ink-saving potential in digital packaging printing was presented as a quantifiable cost lever — demand the saving model in your vendor quotes.
- Colour tolerances must be verified on real substrates (e.g., 350gsm CCNB, E-flute corrugated), not on generic proofing paper.
- The next symposium is scheduled for 23–24 February 2028; treat current Fogra outputs as the reference baseline for 2026–2027 contract cycles.
Extended-gamut printing, AI-driven inspection, and substrate-aware proofing are reshaping how brands buy packaging in 2026. Yet for procurement directors and structural engineers, the question is never “is colour management interesting?” — it is “what numeric spec, what test, and what tolerance goes into the PO?” This guide converts the Fogra symposium agenda into seven concrete engineering and procurement actions, anchored to measurable packaging metrics: ECT/BCT strength, Cobb 60 absorption, ΔE00 colour tolerance, and ASTM D642 compression verification.

1. Replace Spot Density Checks with Image-Based, Spatially Resolved Print Evaluation
A core packaging presentation at the 10th Fogra CMS covered image-based measurement and spatially resolved print evaluation for packaging. The engineering implication: single-point densitometry on a flat patch cannot capture colour variation across a diecut panel, embossed zone, or glue flap. On a folding carton dieline, the same ink film can shift visibly by 0.5–1.5 ΔE00 (typical industry reference range) between a large flood area and a fine reverse-knockout text region, because ink transfer and substrate absorption vary locally.
Procurement action: require vendors to report measurement position maps (minimum 5 points per panel, corners plus centroid, as a typical industry practice) with each colour approval run. TadaPack’s structural prototyping service can supply printed dieline mockups on final substrate before tooling so colour and structure are approved together.
2. Write the ECG 7C Ordering Standard into Your RFQs
The symposium introduced an FFI ordering standard for ECG 7C (seven-colour extended colour gamut), derived from a Fogra research report. ECG replaces dedicated spot inks (Pantone-type) with a seven-ink process set (CMYK plus OGV), delivering three commercial levers: fewer wash-ups, shared press runs across SKUs, and consistent brand colour across multi-plant sourcing.
Procurement action: instead of “match Pantone 485C,” specify “ECG 7C per the FFI ordering standard, tolerance ΔE00 ≤ 2.5 on production substrate.” Typical industry reference: ECG conversion can eliminate 3–6 spot ink stations per SKU family, cutting changeover time and per-order minimum quantities — a material benefit for DTC brands running short-run multipacks.
3. Proof on Real Substrates — or Your Approval Means Nothing
Proofing on real substrates was an explicit session topic at the Fogra symposium. The physics is unforgiving: the same digital front-end file prints measurably different on 350gsm CCNB (coated caustic newsback board, ~0.42–0.48 mm caliper) versus E-flute liner or a C1S cartonboard, because substrate whiteness, Cobb 60 absorption, and surface energy shift the colour gamut.
Q: If the press is calibrated to a Fogra-class characterization, why does my kraft corrugated run still look duller than the proof?
A (3-step): ① Direct metric answer: uncoated kraft liners typically reduce achievable gamut by a visible margin versus coated stock; a contract proof on coated paper is simply not predicting that stock. ② Mechanical reason: ink wicks into uncoated fibres (higher Cobb 60 absorption), scattering light and lowering chroma — a substrate physics effect no ICC re-profile fully cancels. ③ Procurement recommendation: mandate proofing on the actual production substrate (or a characterized simulation of it) and reject proofs made on generic white stock. This is exactly why Fogra’s 2026 programme elevated real-substrate proofing to a headline topic.
4. Audit Ink-Saving Claims in Digital Packaging Printing
Ink-saving potential in digital packaging printing was presented at the symposium as a genuine cost lever. For buyers, “ink saving” must be converted into a verifiable unit-cost line. A hypothetical worked example: a digital carton program consuming 100 units of ink cost index per year could, under a typical ink-saving workflow, see 10–30% ink index reduction (typical industry reference range) through optimized ink limits and under-colour-removal strategies — worth roughly 0.5–1.5% of landed unit cost on ink-heavy designs. Require vendors to state the saving model, the verification method, and whether the saved-ink appearance is covered by your ΔE00 tolerance.
5. AI in Production Workflows: Ask What It Actually Controls
AI in production workflows was another of the symposium’s seven sessions. Practically, AI delivers value where it closes the loop fast: inline camera colour correction, defect classification, and automated make-ready. But procurement should treat “AI-powered” as a process claim requiring audit criteria: what the system measures (image-based, per point 1 above), what it actuates (ink keys / digital heads), and what evidence you receive (inline ΔE00 logs per sheet). TadaPack recommends adding an evidence clause: “vendor provides inline colour measurement logs with each production run.”
6. Colour Is Only Half the Spec — Pair It with Structural Strength Data
A colour-approved carton that fails in transit is a write-off. Every colour spec in this guide should sit beside structural verification:
- ECT per TAPPI T811 / compression per ASTM D642: specify ECT-32 for standard e-commerce shippers, ECT-44 for double-stacked or heavier loads.
- McKee BCT estimate (typical industry formula): BCT ≈ 5.87 × ECT × √(caliper × perimeter). Hypothetical worked example: ECT-44 board, 0.55 cm caliper, 120 cm perimeter → BCT ≈ 5.87 × 44 × √(0.55 × 120) ≈ 1,700 N, against which stacking loads are derated for humidity (typical derating 30–50% in high-humidity coastal warehousing).
- Cobb 60 water absorption: for corrugated destined for 30-day ocean transit, keep Cobb 60 within typical spec ≤ 100–125 g/m² to limit fibre softening and glue-line delamination.
- Transit validation: ISTA 3A General Simulation for parcel DTC shipments; ASTM D4169 for distribution-cycle loads.
Verify structural numbers interactively with TadaPack’s free calculation tools at tadapack.com/tools before committing board grades.
7. Lock the Whole Package into a Verifiable Colour + Structure SOP
Consolidate the above into a four-step pre-production SOP:
Step 1 — Substrate lock: freeze substrate grade, caliper, and Cobb 60 spec (e.g., 350gsm CCNB, 0.45 mm ±0.03 mm) before any colour profiling; condition samples at 23°C ± 1°C, 50% ± 2% RH per ISO 187.
Step 2 — Colour contract: choose ECG 7C per the FFI ordering standard or spot-ink route; set ΔE00 tolerances (solids ≤ 2.5, greys ≤ 1.5 — typical industry reference values) and require proofs on real substrate.
Step 3 — Dieline & tooling: release factory dielines with ±0.15 mm die registration tolerance, creasing matrix matched to board caliper, and glue-flap knockouts kept clear of measurement zones.
Step 4 — Verification: acceptance per measurement position map (5+ points/panel), inline ΔE00 logs, plus structural sign-off via ASTM D642 compression and ISTA 3A transit pre-ship.
Pre-PO checklist — tick every item:
- Substrate grade and caliper specified with tolerance (±0.03 mm typical)?
- Proofing substrate = production substrate, in writing?
- ECG 7C reference to the FFI ordering standard stated in the RFQ?
- ΔE00 tolerance and measurement point map defined?
- Ink-saving model quantified for digital runs?
- ECT grade, McKee BCT check, and Cobb 60 limit documented?
- ISTA 3A / ASTM D4169 transit validation scheduled?
- Colour evidence deliverable (inline logs) written into the contract?
Wrap-up: The 10th Fogra Colour Management Symposium signals where industrial colour control is heading: spatially resolved, substrate-true, standards-backed, and AI-assisted. Convert each signal into a numeric PO clause — measurement maps, FFI ECG 7C ordering, real-substrate proofs, quantified ink-saving — and pair it with ECT/BCT/Cobb structural verification. TadaPack’s structural prototyping and calculation tools let you approve colour and structure in one engineering cycle; the next Fogra benchmark lands 23–24 February 2028, and your 2026–2027 supplier contracts should already meet it.
Recommended Engineering Reading
[TOOLS] Featured Engineering & Calculation Tools
Explore 70+ Packaging Tools ➔Foil Stamping Area & Cost Calculator
Estimate hot foil stamping area, foil consumption, and die tooling costs.Imposition & Sheet Utilization Optimizer
Optimize parent sheet imposition layouts to minimize off-cut paper waste.
