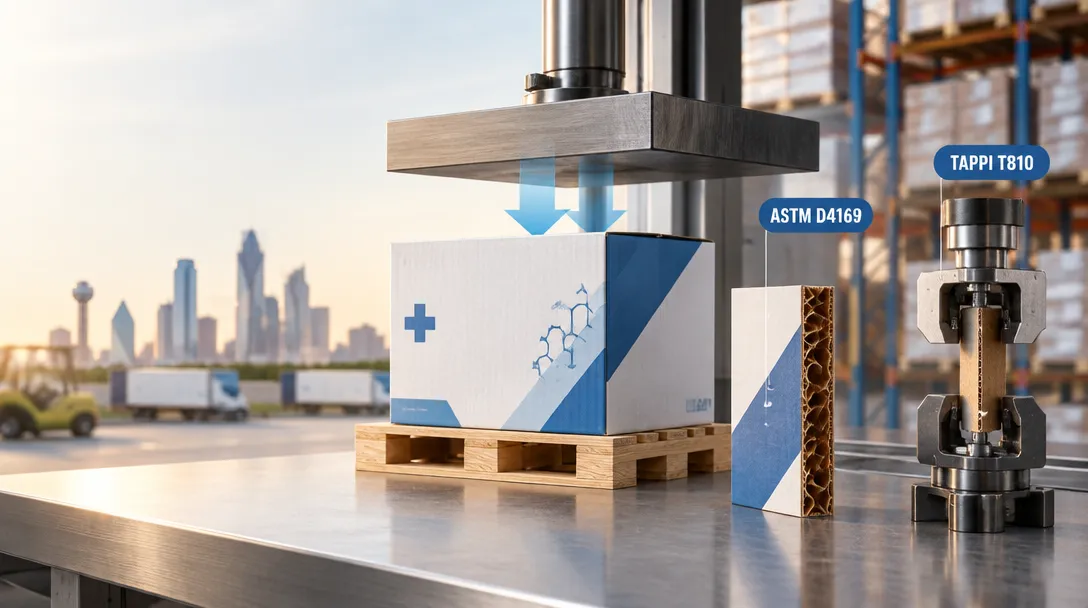
For short-run pharmaceutical packaging routed through Dallas–Fort Worth, qualify the complete shipper system with an ASTM D4169 distribution test plan and use TAPPI T810 to assess corrugated board burst strength. T810 is a material test, not proof of route performance; choose board, internal protection, and test conditions for the actual product and distribution hazards.
Digital printing can make short production runs commercially practical, but rapid artwork changes do not reduce the engineering burden on a pharmaceutical shipper. A carton that passes a board-strength check can still fail through vibration-driven movement, compression, closure opening, or damage to the product-contact package. For DFW distribution, procurement and engineering teams should treat the test specimen as the packed system—not a flat board sample—and distinguish material screening from distribution qualification.
This guide focuses on the boundary between the two named protocols: ASTM D4169 evaluates shipping-unit performance under a selected distribution-cycle test plan, while TAPPI T810 measures corrugated board burst strength. Neither standard alone establishes pharmaceutical regulatory compliance, product stability, or suitability for every parcel or pallet route. The test plan must reflect the actual packaging configuration, shipment mode, and acceptance criteria.
What do ASTM D4169 and TAPPI T810 each prove for pharma packaging?
ASTM D4169, Standard Practice for Performance Testing of Shipping Containers and Systems, provides a framework for evaluating a shipping unit against distribution hazards. The responsible team selects the distribution cycle, assurance level, test sequence, and acceptance criteria appropriate to the shipping environment. Those choices matter: a test plan selected for one handling profile should not be represented as universal qualification for all parcel, less-than-truckload, or palletized shipments.
TAPPI T810, Bursting Strength of Corrugated and Solid Fiberboard, is a board-level test. It indicates resistance to a specified bursting action under the method; it does not directly measure box compression, edge-crush strength, closure integrity, or cushioning effectiveness. Treat a T810 result as one input to material control and supplier qualification. It cannot replace a filled-shipper test when the purchasing question is whether the package will protect product through distribution.
ECT is another distinct measure: Edge Crush Test reports resistance to edgewise compression of corrugated board. ECT-32 or ECT-44 may be used as board specifications where appropriate, but neither designation independently defines a finished shipper’s performance. Box dimensions, flute construction, joints, converting quality, orientation, package mass, and environmental exposure all affect the outcome. Do not infer a guaranteed burst value from an ECT grade, or a guaranteed box compression value from a burst result.
For digital short runs, verify that the tested sample matches production intent: substrate and flute combination, board direction, print coverage, score and crease geometry, adhesive, closure, and insert. Digital print setup can differ from a production sample made by another process; evaluate whether ink coverage, coating, or finishing changes fold behavior or surface friction. If the pharma product has a primary container, the shipping test should include the relevant primary pack and internal components, with sensitive product or stability testing handled under the applicable quality system.
How should buyers qualify a short-run shipper for Dallas–Fort Worth distribution?
Start by mapping the distribution system rather than assuming that “DFW” represents one fixed hazard profile. A shipment may be parcel-delivered, consolidated, transferred between facilities, or moved as part of a palletized load. The route, carrier service, package orientation, handling frequency, and stacking conditions determine which ASTM D4169 distribution cycle and test details are appropriate. Request the route and handling assumptions from the logistics owner; record them in the packaging specification so the test remains traceable to the intended use.
Define the shipping unit precisely. Record the external dimensions, gross mass, number of units per shipper, closure method, internal restraint, and product fragility or leakage concerns. Corrugated board selection should consider ECT, flute construction, caliper, and converting quality together. E-flute and B-flute can support different print, stiffness, and cushioning trade-offs; C-flute or combined constructions may be considered where load or handling requirements justify them. These are design choices, not universal prescriptions. A larger or heavier shipper can also affect parcel dimensional-weight charges; assess the carrier’s current rules and package dimensions rather than assuming a specific penalty or rate.
Build acceptance criteria before testing. Examples include no unacceptable product damage, no closure opening, no loss of containment, and no structural failure that prevents intended handling. Define what “unacceptable” means for the product and quality system. For example, a cosmetic crease may be acceptable for an outer shipper but not if it compromises a sterile barrier or creates a traceability problem. A test report should identify specimen configuration, conditioning, test sequence, observed failures, and disposition; do not claim a pass merely because the carton appears intact after one isolated test.
Moisture exposure can reduce corrugated performance and affect adhesive or print finishes. If the distribution profile includes moisture risk, set a suitable conditioning and test approach and evaluate whether coatings or other barriers are compatible with the recycling and regulatory requirements of the markets served. A Cobb 60 result is a water-absorption measurement under its defined method, not a direct guarantee against transit delamination. Specify a relevant limit only after confirming the board, coating, and failure mode; do not apply a generic threshold without product-specific evidence.
When should a procurement team schedule testing and release?
Short-run production often compresses the time available for design approval. The efficient response is not to skip qualification, but to separate early structural decisions from final release evidence. Use CAD and prototypes to resolve dimensions, fit, closure, and insert retention before ordering the production run. Then test representative packed samples made with production-intent materials and converting. If the print file, board grade, insert, closure, or shipper dimensions change after testing, assess whether the change affects the evidence and repeat the relevant evaluation when necessary.
The following timeline is a project-planning sequence, not a claim that ASTM D4169 or TAPPI T810 has a new regulatory effective date. No new effective date or revision is asserted here. At the current planning snapshot, 2026-11-12, buyers should confirm the applicable standard editions and any customer-specific requirements directly with their quality and testing teams before issuing a purchase specification.
- 2026-11-12 — Planning snapshot: Confirm applicable ASTM D4169 and TAPPI T810 editions, customer requirements, and the current DFW distribution profile; this date is a planning reference, not a standards-change date.
- Before production artwork release — Design qualification: Freeze the shipping configuration, confirm board and internal components, and resolve fit and closure risks with a structural prototype.
- Before purchase-order release — Performance evidence: Complete the agreed material checks and distribution testing on representative packed samples; record results and deviations.
- At change approval — Requalification decision: Review any change to dimensions, board, insert, closure, print finish, or route and determine whether new testing is needed.
Commercial quotations should distinguish setup and prototyping costs from recurring unit costs. In short runs, artwork and tooling strategy, board availability, converting steps, and test-sample quantities can influence unit economics. Avoid comparing bids on unit price alone if one offer excludes structural development, test specimens, or specified materials. TadaPack can support custom structural packaging and prototyping so buyers can evaluate fit and configuration before production commitment; use its calculation tools at https://tadapack.com/tools to support preliminary packaging calculations, then verify the final design with representative samples and the required test protocol.
What should the purchase specification and test checklist require?
Write the specification so a converter, testing laboratory, and receiving quality team can interpret it consistently. Name the actual standards and distinguish the test purpose: TAPPI T810 for board burst-strength assessment where required, and ASTM D4169 for the agreed shipping-unit performance evaluation. Do not put an unsupported pass value into a purchase order simply because it appears in an older supplier document. Establish values from the product’s risk, package design, customer requirements, and documented qualification evidence.
For a DFW-bound shipper, include route assumptions and handling units in the specification. If the same pack will serve multiple US or European markets, identify the intended distribution profiles separately and confirm any additional regional packaging, labeling, or environmental obligations with the responsible compliance team. A successful ASTM D4169 test does not establish compliance with pharmaceutical rules or packaging-waste requirements; those are separate assessments. Similarly, a recyclable-material claim requires its own market-appropriate substantiation.
- [ ] Identify the product, primary container, shipping configuration, gross mass, dimensions, closure, and internal protection.
- [ ] Specify the intended DFW route and handling mode, and have the responsible engineering team select the applicable ASTM D4169 distribution cycle, assurance level, sequence, and acceptance criteria.
- [ ] State whether TAPPI T810 burst testing is required for board control, supplier qualification, or another documented purpose; do not use it as a replacement for shipping-unit testing.
- [ ] Record the corrugated construction and board requirements, including any ECT grade such as ECT-32 or ECT-44, without treating the grade as a complete performance guarantee.
- [ ] Test representative, production-intent packed samples and document configuration, conditioning, observations, failures, and disposition.
- [ ] Define change control for board, flute, dimensions, insert, adhesive, closure, print finish, and distribution route.
- [ ] Review dimensional-weight exposure, material claims, and market-specific regulatory obligations independently of physical distribution test results.
- [ ] Use structural prototyping and the TadaPack calculation tools for early design work, then confirm decisions through the approved qualification process.
Procurement decision: Approve a short-run pharma shipper only when its material specification, packed configuration, and distribution evidence align. TAPPI T810 helps characterize board burst strength; ASTM D4169 addresses the performance of the shipping unit under a selected distribution simulation. Neither is a stand-alone guarantee, and neither should be substituted for the other.
Recommended Engineering Reading
[TOOLS] Featured Engineering & Calculation Tools
Explore 70+ Packaging Tools ➔Box Compression (BCT) Calculator
Predict box compressive limit and stacking safety factors via McKee formula.Edge Crush Test (ECT) Calculator
Calculate linerboard ring crush and composite ECT ratings for optimal board specs.
Frequently Asked Technical Questions (FAQ)
Does TAPPI T810 prove that a pharmaceutical shipper will survive DFW distribution?
Should a buyer specify ECT-32 or ECT-44 for a short-run pharma carton?
What must an ASTM D4169 test plan state for DFW distribution?
Does passing ASTM D4169 establish pharmaceutical regulatory compliance?
