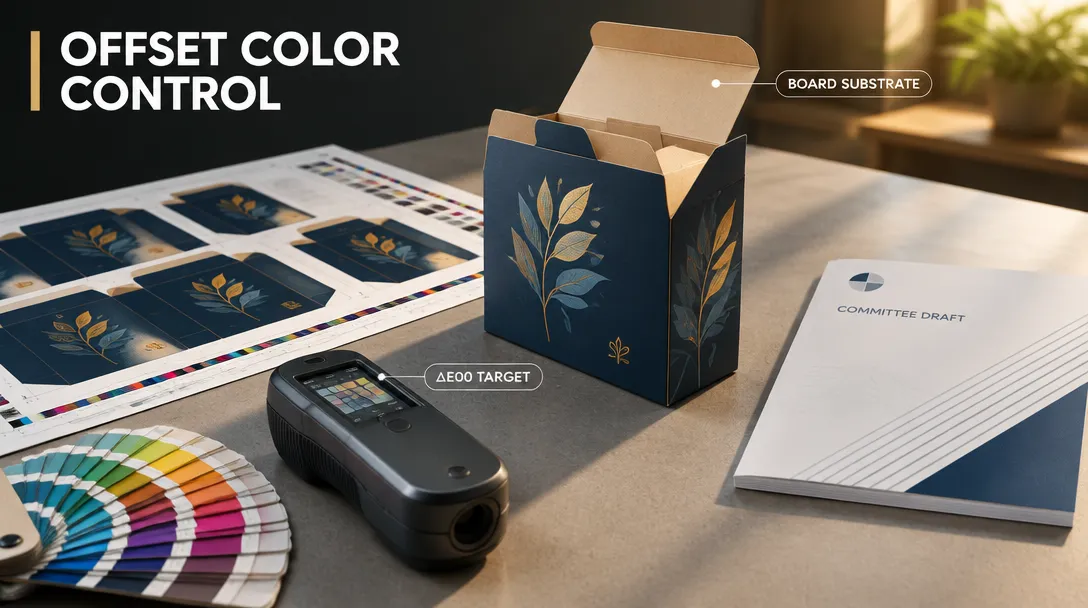
ISO/CD 12647-2 is the fourth edition under development at committee draft stage, not yet a final replacement for ISO 12647-2:2013. Keep colour approval, substrate identification and packaging performance criteria explicit in the job specification, and require suppliers to confirm any changes when the final edition is published.
What the committee draft means for packaging buyers
Offset printing standard ISO 12647-2 has advanced to committee draft (CD) within ISO/TC 130. For buyers, this is a standards-development milestone—not evidence that a new edition is already published, or that current production should be requalified against undisclosed requirements. The public ISO document identifies a fourth edition under development and states that the existing 2013 edition specifies process parameters and values for four-colour sheet-fed and web-fed offset, excluding coldset offset lithography on newsprint.
The published edition spans colour separation, proof production, printing-forme preparation, OK print and production printing on commercially available substrates. It applies to cardboard material for packaging and to heat-set, infrared and ultraviolet drying. It also provides references for quality assurance and quality management. Those are useful boundaries for procurement: a carton printer can be asked to describe its process controls across the complete production chain, but the CD-stage notice alone does not establish new numerical targets.
For packaging teams, keep three decisions separate. First, specify visual and instrumental colour acceptance for the actual board and finish. Second, specify structural and distribution performance independently: print conformity does not prove a carton survives stacking, vibration or drops. Third, manage revision risk by recording the standard edition and the approved customer-specific criteria in the technical agreement. Do not describe a CD as a published requirement or presume that a draft’s eventual content is known.
Translate the process scope into measurable job controls
A useful carton specification follows the production sequence rather than stopping at a brand colour name. The separation and proof stage should identify the intended artwork version, colour reference and proof approval method. The printing-forme and press stages should record the approved process, substrate, drying method and production reference. The run approval should connect the signed or otherwise traceable OK print to the production lot and finished packaging inspection.
There is no single universal tolerance in the public source facts supplied for this review. Accordingly, the table below deliberately separates ISO scope from typical engineering reference values. Values are examples for a buyer-printer discussion, not ISO 12647-2 limits, acceptance criteria, or TadaPack test results. Establish final limits with the printer using the actual board, ink system, coatings, viewing conditions and measurement method.
| Control point | What the buyer should define | Typical industry reference values | Governing Standard / Test Protocol |
|---|---|---|---|
| Colour target and approval | Artwork version, colour references, proof status and approval authority | Illustrative ΔE00 target band: 2–5, agreed by project; not an ISO limit stated here | ISO 12647-2:2013 process scope; contract defines acceptance |
| Substrate identity | Board grade, mill or approved equivalent, side to print and surface finish | Typical carton board basis weights may span roughly 250–450 g/m²; select for structure and print surface | ISO 12647-2:2013 includes commercially available substrates and packaging cardboard |
| Drying route | Heat-set, infrared or ultraviolet process as applicable; confirm compatibility with finishing | No universal setpoint: printer validates ink, coating and line conditions | ISO 12647-2:2013 scope includes these drying methods |
| Press-run approval | OK print reference, approved sample retention and deviation escalation | Illustrative sampling: first-off approval plus documented in-run checks, frequency set by risk | ISO 12647-2:2013 process stages; quality plan agreed between parties |
| Finished pack strength | Separate structural requirement for compression, vibration and distribution hazards | ECT-32 or ECT-44 may be candidate corrugated grades, not guaranteed finished-box performance | ASTM D642 for container compression; ISTA 3A where the parcel distribution profile fits |
Colour numbers need context. A ΔE value is meaningful only when the parties agree the colour space, calculation method, measurement geometry, backing, instrument setup and sampling location. Printed board also varies with whiteness, absorbency, coating, ink film and drying. A numeric target borrowed from coated paper may not predict appearance on uncoated or highly absorbent packaging stock. Treat a proposed band as a negotiated reference, validate it on production-representative board, and retain an agreed physical reference where appearance is commercially critical.
Choose substrate and print route around the finished carton
Substrate selection is a coupled print-and-structure decision. A coated cartonboard can support fine image reproduction, while the board’s stiffness, caliper, crease behaviour and moisture response determine converting and pack performance. Corrugated packaging adds flute geometry and liner properties; an offset-printed litho label or laminated top sheet does not make the underlying corrugated board immune to compression or moisture damage. Specify the actual construction rather than relying on a surface description such as “premium board.”
For folding cartons, request the board grade and nominal basis weight, print side, coating or laminate, grain direction where relevant, and any approved substitute. For corrugated packs, request the liner/flute construction and ECT grade where the supplier uses that measure. ECT-32 and ECT-44 are common commercial grade designations, but the grade alone does not determine box compression strength. Box dimensions, perimeter, board caliper, converting quality, humidity and loading configuration all influence performance.
The McKee relationship is often used as a preliminary estimate of box compression from ECT, box perimeter and board caliper. It is a screening calculation, not a performance guarantee: real cartons can fail earlier because of score-line damage, poor joints, print/lamination effects, eccentric stacking or environmental exposure. A hypothetical worked example should therefore use a supplier’s stated ECT and measured dimensions, then apply a clearly disclosed safety factor and validate the resulting design with representative testing. Never convert an estimate into a guaranteed BCT claim without a test protocol and defined conditioning.
Moisture management also belongs in the substrate conversation. Cobb 60 describes water absorptiveness over a 60-second test interval; it is useful when evaluating paper or board surfaces, but a single Cobb value does not by itself predict a complete carton’s transit life. Ask whether a barrier treatment is compatible with print, adhesive, recycling pathway and local requirements. For sensitive applications, request evidence for PFAS-free coating claims and define the precise claim scope; do not infer chemical composition from a marketing term.
Print finish and structural conversion must be qualified together. Varnish, aqueous coating, UV coating, lamination, foil and embossing can alter friction, crease cracking, foldability, glue adhesion and recyclability. Ensure the approved print sample is representative of the converted package, not merely a flat press sheet. TadaPack can support custom structural packaging development and prototyping so artwork, dieline, substrate and pack performance are reviewed as one system.
Connect print approval to distribution performance and cost
For DTC shipments, the printed exterior is part of the shipper’s protection system only when the package is designed and tested for that role. ISTA 3A is a general simulation test procedure for individual packaged-products shipped through parcel delivery systems; ASTM D4169 provides a distribution-cycle approach for shipping containers. Select the protocol based on the actual route, package type, product fragility and handling profile. Do not claim “ISTA compliant” merely because a design passed an unrelated vibration or drop test.
Structural qualification should use the finished pack, including print and finishing operations. A practical verification plan identifies the product mass and dimensions, packed orientation, closure method, distribution test profile, pass/fail criteria and sample conditioning. Compression needs special attention for cases exposed to stacking; a short parcel test does not automatically represent warehouse dwell or pallet loads. If moisture is a credible hazard, include a justified conditioning or exposure plan and inspect for board softening, delamination, ink scuffing and adhesive failure.
Procurement cost-down should compare total delivered cost rather than print price alone. A lighter board may reduce material and freight cost but increase damage risk; extra coating may improve scuff resistance yet add cost or complicate recovery; a larger carton may trigger higher dimensional freight charges. For each proposed change, compare unit price, setup and tooling, expected scrap, shipping cube, product protection and end-of-life constraints. Use a controlled pilot and record the approved construction so that substitutions do not silently reset the baseline.
As an illustrative calculation, if a carton’s outside dimensions are each increased by 5%, its cubic volume becomes 1.05 × 1.05 × 1.05 = 1.1576, or about 15.8% more volume. This is geometry, not a carrier surcharge prediction: actual dimensional billing depends on carrier rules, service and package measurements. TadaPack’s online calculation tools at tadapack.com/tools can support early comparison, while final freight and structural decisions should be verified against the selected carrier and test plan.
For print procurement, the most effective cost-control document is a shared specification containing substrate, approved colour reference, print and drying process, finish, conversion drawing, structural criteria, sampling plan and change-control procedure. Include a statement that ISO/CD 12647-2 is under development and that the applicable contractual edition remains the one explicitly named in the order until the parties agree otherwise. When the final edition is available, assess its published scope and transition implications with the printer rather than assuming automatic adoption.
Use revision control to prevent specification drift
During a draft transition, the risk is less about an immediate press change and more about inconsistent assumptions among brand, printer, converter and procurement. One supplier may quote a current published edition, another may refer informally to committee discussions, while the packaging team is focused on a colour tolerance or substrate that is not stated in either reference. Resolve that ambiguity in the purchase specification: name the applicable edition, define customer-specific acceptance requirements, and require written notice before a process or material substitution.
Keep colour and package performance records distinct but linked. A press approval record should identify the job, substrate, finish and approved appearance reference. A structural record should identify the package construction, product configuration, closure and distribution protocol. Linking them by drawing revision and production specification allows a colour change, board substitution or coating update to trigger the correct review without incorrectly treating every artwork revision as a complete structural requalification.
In 2026, the safe procurement position remains to monitor the ISO/TC 130 revision status and obtain the final published text before adopting new obligations. The supplied ISO page establishes committee-draft status and the scope of the 2013 edition; it does not provide draft requirements, publication timing or transition rules. Ask the printer to confirm current certification or process-control claims independently, and avoid quoting unpublished draft thresholds in a tender.
Engineering takeaway: ISO 12647-2 addresses offset process control, including packaging board; it does not replace the need for a complete structural specification. Tie the approved print condition to the actual converted pack, then qualify compression and distribution performance against the intended supply chain. For custom dielines, short-run prototypes or a cost-down review, TadaPack can help coordinate structural design and packaging calculations before production tooling is committed.
Frequently asked questions about ISO 12647-2
Is ISO/CD 12647-2 already mandatory for carton production?
No. The cited ISO page identifies the fourth edition as under development at committee draft stage. The published ISO 12647-2:2013 remains the edition described in the source; buyers should state the applicable contractual edition and wait for the final publication before treating revised provisions as requirements.
Does ISO 12647-2 cover offset-printed packaging board?
Yes. The published 2013 edition applies to printing on cardboard material for packaging and covers four-colour sheet-fed and web-fed offset printing, excluding coldset offset lithography on newsprint. Its stated scope includes the stages from colour separation and proof production through OK print and production printing.
Does a colour approval prove a carton will survive parcel shipping?
No. Print approval establishes appearance or process acceptance, while parcel performance requires a separate test plan for the finished package. Depending on the distribution profile, consider ISTA 3A or ASTM D4169 and define product configuration, conditioning and pass/fail criteria.
Can we set a universal ΔE tolerance for all printed cartons?
No universal tolerance is established by the source facts cited here. Agree the measurement method, substrate, finish, sampling locations and acceptance band with the printer; validate the reference on production-representative packaging rather than transferring a paper target without qualification.
What should procurement put in a 2026 offset-carton RFQ?
Name the contractual standard edition, substrate and approved alternatives, colour reference and measurement agreement, drying and finishing route, OK-print approval, conversion drawing, structural criteria, test protocol and change-control requirements. Ask suppliers to flag any proposed change resulting from the eventual final edition.
Recommended Engineering Reading
[TOOLS] Featured Engineering & Calculation Tools
Explore 70+ Packaging Tools ➔Foil Stamping Area & Cost Calculator
Estimate hot foil stamping area, foil consumption, and die tooling costs.Imposition & Sheet Utilization Optimizer
Optimize parent sheet imposition layouts to minimize off-cut paper waste.
