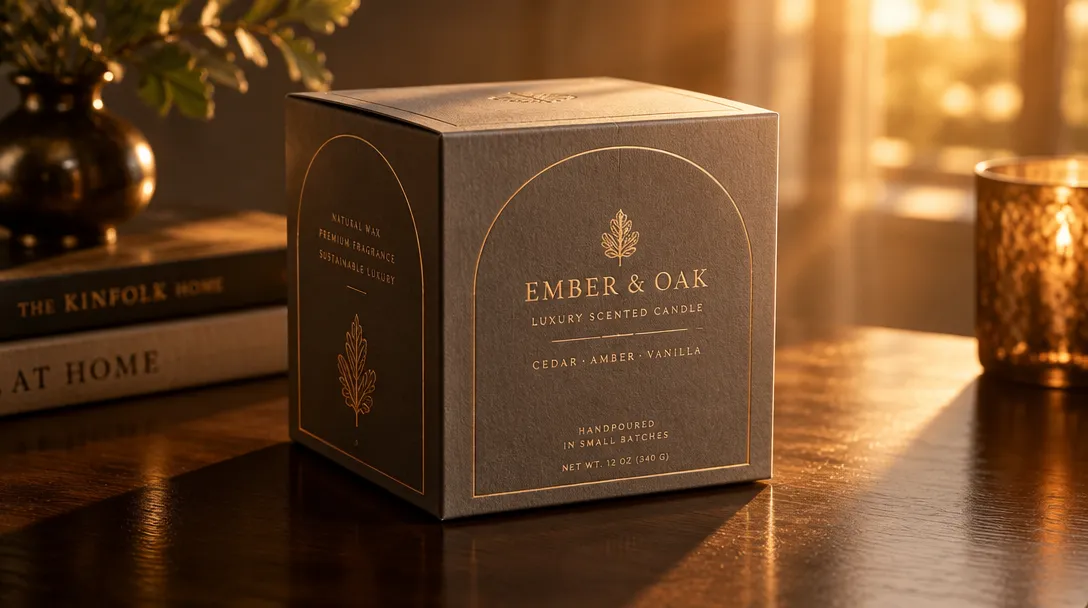
Candle packaging at wholesale scale fails for two engineering reasons: under-specified board compression (BCT below the stacked load of a 40-inch pallet column) and glass jar migration inside the primary carton. Specify ECT-32 minimum for single-wall shippers carrying 12-16 oz jars, validate to ASTM D642 and ISTA 3A, and derate stacking strength 30-40% for 30-day ocean transit humidity.

What Does ‘Candle Packaging Wholesale’ Actually Mean in 2026 Procurement Terms?
Wholesale candle packaging means contract-manufactured primary and secondary packaging procured at MOQ tiers — typically 1,000-5,000 units for digitally printed folding cartons and 5,000-10,000 for rigid grayboard sets — rather than retail or short-run digital quantities. The distinction is structural, not just commercial: at wholesale volumes you move from digital toner to offset litho-laminated or direct flexo processes, where ΔE color tolerance of ≤2.0 against a proofed standard (per ISO 12647-2 practice) becomes contractually enforceable. The 2026 DTC candle market is crowded and price-compressed, which pushes buyers toward cost-per-unit engineering rather than boutique finishes — and that means your real decision variables are board grade, flute selection, tooling amortization, and freight class.
Which Board and Flute Construction Should I Specify for Glass Candle Jars?
Match the shipper flute to the gross pallet load, not to the jar alone. A 12 oz glass-filled jar plus wax typically weighs 450-600 g; a 16 oz format reaches 750-900 g. For a master case of 12 units, a single-wall C-flute ECT-32 RSC is generally adequate for domestic US LTL distribution, while export ocean programs benefit from ECT-44 C-flute or BC double-wall to survive container sweat and multi-tier stacking. For the primary carton, 350gsm CCNB (clay-coated newsback) is the volume-workhorse for sleeve-style candle boxes, while 1.5-2.0mm grayboard wrapped in printed paper defines the rigid ‘luxury’ tier for 3-wick formats. Insert engineering matters as much as board: corrugated or molded pulp inserts with ±0.5mm cavity tolerance prevent jar migration, which is the #1 damage mode — glass-on-glass contact during ASTM D4169 truck vibration sequences.
Q: If the McKee formula derives BCT from ECT, why do large retail POs still mandate box compression testing?
A: Because McKee is a statistical estimate with ±10-15% error, not a substitute for measurement. Under ASTM D642, a physical BCT test captures real-world variables — warp, print-induced delamination, humidity conditioning — that the formula ignores. Procurement recommendation: use McKee for initial board selection, then require ASTM D642 validation on the production board lot before releasing the PO, and stack-test to ISTA 3A sequences for the full packed case.
What Is the True Unit Cost of Wholesale Candle Packaging — Board, Tooling, or Freight?
Freight and tooling usually dominate, not board price. A hypothetical worked example: a 350gsm CCNB sleeve might cost $0.28-0.42/unit at 5,000 MOQ, while a 1.5mm grayboard rigid box with wrap runs $0.85-1.40/unit — but the rigid box’s larger flat-packed footprint can push you over dimensional-weight breakpoints. Under 2026 carrier dim-weight rules (divisors in the 139-166 range depending on service), an oversized master carton can add $1.50-3.00 per case in freight penalties, dwarfing the $0.20/unit you saved on board. Tooling (die-cutting dies, ~$150-450 for a folding carton die; emboss/foil plates higher) is amortized across the run, so at 5,000 units a $300 die adds $0.06/unit — negligible, but at 1,000-unit short runs it becomes $0.30/unit and reshapes the material decision. Also budget for FBA-specific constraints: Amazon prep and SIOC (Ships In Own Container) eligibility effectively requires ISTA 6-Amazon.com-grade overbox performance, and non-compliant case dimensions trigger FBA prep fees. Verify your pallet configuration and dim-weight exposure with TadaPack’s free calculation tools at https://tadapack.com/tools before locking a dieline.
How Do I Validate Candle Packaging Against Transit and Compliance Standards?
Validate in three layers: material, packed-case, and regulatory. Material layer: caliper per TAPPI T411, burst per TAPPI T810, ECT per TAPPI T811, with conditioning at 23°C ± 1°C and 50% ± 2% RH per ISO 187 practice. Packed-case layer: ASTM D642 compressive resistance for stacking, ISTA 3A General Simulation for parcel e-commerce lanes, ASTM D4169 for LTL distribution cycles. Regulatory layer: for EU-bound products, EU Regulation (EU) 2025/1892 (the recast PPWR) tightens recyclability and packaging minimization requirements — your grayboard and corrugate must be demonstrably recyclable in the destination stream, and any ‘recyclable’ claim in US marketing must be substantiated per FTC Green Guides (16 CFR Part 260). Avoid PFAS-containing grease barriers on any food-adjacent candle components (tealight cups, wax melts); specify PFAS-free barrier coatings explicitly on the PO.
What Is the Step-by-Step SOP for Ordering Wholesale Candle Packaging?
Step 1 — Define the load case: document jar weight, wax fill mass, and final packed-case gross weight; derive pallet stack height and tier count to compute the required BCT with a 3-5x safety factor for warehouse stacking (per ASTM D4169 assurance-level thinking).
Step 2 — Prototype structurally, not cosmetically: request short-run prototyping of the dieline with production-equivalent board (same ECT rating and caliper, ±0.15mm tolerance), and drop-test the prototype pack before committing to a die; TadaPack’s custom structural prototyping service produces production-matched samples for this exact gate.
Step 3 — Lock spec sheet with governing standards: the PO should cite board ECT, caliper per TAPPI T411, glue-lap width (typically 32-38mm), crease-rule specifications for the flute, and acceptance tests (ASTM D642, ISTA 3A) so QC disputes have contractual anchors.
Step 4 — Pilot then scale: run 1-2% of the MOQ as a pilot lot through your actual fulfillment flow, inspect flap alignment and adhesive bond, then release the balance; this catches registration or warp issues at $0.02/unit exposure rather than post-shipment.
What Are the Most Common Wholesale Candle Packaging Defects and Fixes?
Defect 1 — Grayboard warping on rigid boxes: root cause is moisture gradient between wrap paper and board during lamination or ocean transit; board absorbs humidity asymmetrically and bows. Corrective action at floor level: require symmetric wrap lamination (print on both faces or a balancing liner), condition board per ISO 187 before converting, and specify sealed pallet wrap plus desiccant for ocean containers; Cobb 60 water absorption above ~35 g/m² on the liner is a red flag for transit delamination risk.
Defect 2 — Flap popping / glue-lap failure on RSC shippers: root cause is hot-melt adhesive applied below the open-time window or cold-set glue under-cured in humid warehouses. Fix: verify adhesive application temperature against the adhesive TDS (typically 160-180°C application for EVA hot melts), check glue-lap compression at the nip, and if cases open on the pallet, upgrade the bottom flap pattern from 5th-panel to H-seal or move to BCT-validated ECT-44 stock.
Q: Should I single-source primary cartons and shippers from one supplier or split the award?
A: Single-source when the shipper must nest the primary exactly (cavity tolerance ≤0.5mm), because cross-vendor tolerance stacking is the leading cause of insert failure; split the award when volumes justify it and both specs are independently standard-compliant. Recommendation: pilot with one supplier, then dual-source commodity sleeves once dielines are frozen.
Does Ocean Freight Change My Candle Packaging Specification?
Yes — treat every export lane as a humidity-loaded compression case. Across 30-day Pacific and Atlantic ocean transits, container sweat can drive interior RH above 85-90%, derating corrugated stacking strength by 30-40%; combined with European inland hubs such as Rotterdam multimodal rail/road transfers and Southern California intermodal moves into the Inland Empire (ONT8/LGB3 corridors), your effective BCT is far lower than the lab number. Engineering rule: for export candle programs, spec ECT-44 or BC double-wall, add a corrugated or poly pallet top-cap and edge boards to shift vertical loads off the primary cartons, and confirm final stack loads against your destination DC’s rack configuration. Run the derated stack-height math against your case dimensions using TadaPack’s free calculation tools at https://tadapack.com/tools before approving the dieline.
Recommended Engineering Reading
[TOOLS] Featured Engineering & Calculation Tools
Explore 70+ Packaging Tools ➔Box Compression (BCT) Calculator
Predict box compressive limit and stacking safety factors via McKee formula.Edge Crush Test (ECT) Calculator
Calculate linerboard ring crush and composite ECT ratings for optimal board specs.
