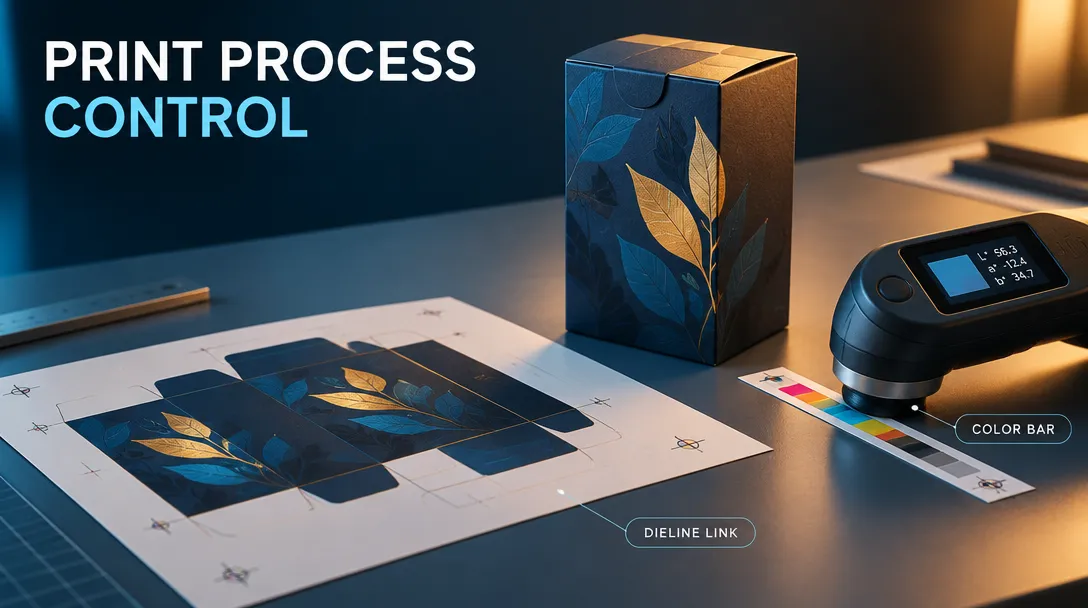
ISO 12647-1:2013 establishes a minimum set of primary process-control parameters for specifying production-print appearance and related technical properties; it does not, on the evidence summarized here, supply package-specific dieline or transit-performance limits. Buyers should use it to frame print-condition communication, then separately approve substrate, converting tolerances, and distribution testing against their packaging specification.
For packaging procurement, print control is a handoff problem as much as a press problem: an approved visual target must survive substrate choice, finishing, die-cutting, folding, and shipment. The ISO source is the scope anchor; the practical controls below are TadaPack engineering guidance, not additional findings attributed to ISO.
What does ISO 12647-1 say about process-control parameters?
ISO 12647-1:2013 defines and explains the minimum set of primary process-control parameters required to uniquely specify the visual characteristics and related technical properties of process-specific production prints. It also covers process-independent simulations of fully characterized printing conditions. The document is published by ISO under Technical Committee ISO/TC 130, is the third edition, contains 17 pages, and is confirmed as an International Standard. These are the source facts used in this review; they should not be expanded into unsupported claims about particular packaging press settings or acceptance tolerances.[1]
For a buyer, the important distinction is between a control framework and a finished-packaging specification. A print condition describes what the parties need to communicate and control for a print process. A converted carton additionally has a board grade, flute or caliper, coating and finish, die-line geometry, crease behavior, adhesive system, and distribution environment. Those are connected engineering variables, but they are not interchangeable.
Accordingly, do not put an assumed color tolerance, registration limit, or board-performance threshold into an ISO 12647-1 claim unless the actual applicable specification supports it. Instead, agree measurable acceptance criteria with the printer and converter, identify the measurement method, and record who approves the reference. Treat any values in a purchase order as contractual project requirements, not as numbers supplied by this ISO overview.
Who and what should a packaging buyer include in scope?
Include the brand or artwork owner, print supplier, converter, structural engineer, and procurement lead in one approval route. The print supplier needs the intended process and substrate information; the converter needs final artwork mapped to a controlled dieline; procurement needs the approved construction and acceptance criteria tied to the ordered SKU. If a print simulation is part of the workflow, state which characterized condition it represents and how the simulation will be reviewed.
Keep the package specification in linked layers. The print layer records artwork revision, intended print process, proof/reference approval, and agreed inspection method. The converting layer records board construction, flute where relevant, nominal caliper, dieline revision, crease and glue design, and permitted manufacturing variation. The performance layer records the distribution risks and selected test plan. For shipping cases, ECT-32 and ECT-44 are common grade designations buyers may encounter; they are not print-control parameters and should not be treated as guaranteed box-compression results. Compression also depends on dimensions, board construction, joints, humidity, and workmanship.
Where e-commerce distribution matters, specify a relevant protocol rather than relying on print approval as evidence of shipment readiness. ISTA 3A and ASTM D4169 are examples of distribution-test frameworks that may be selected by a project team. Confirm the current applicable protocol, distribution profile, sample configuration, and pass criteria with the test provider or customer. Do not infer a test outcome from a material grade alone.
Which dates matter, and what does the source timeline establish?
The source facts identify a dated record and the document’s edition status. They do not establish, in the evidence available for this review, a future compliance deadline or a packaging-specific effective date. Procurement teams should therefore distinguish the source record date below from their own contract milestones and any independently verified standards updates.
- 2024-07-01 — Date attached to the supplied source key facts; this is not presented as an effective date or a new compliance deadline.
The standard is identified in the source as ISO 12647-1:2013, third edition, and confirmed as an International Standard. Before a new program or supplier change, verify the applicable edition and status directly through the official ISO page rather than assuming the record date signals a revision.
What should procurement and engineering do now?
Build a control plan around decision points rather than a vague instruction to “match the sample.” First freeze the artwork and dieline as separate controlled files. Then agree how print appearance is judged on the specified production substrate, including the reference, viewing and measurement arrangements chosen by the parties. Finally, approve converting and distribution performance separately. This prevents a visually acceptable proof from being mistaken for a validated shipping package.
For a hypothetical packaging program, suppose a buyer is comparing ECT-32 and ECT-44 cases. Those labels are candidate board-strength grades, not a complete selection rule. The engineer should evaluate the actual box dimensions and loading, consider stacking and moisture exposure, and determine whether a project-specific compression or distribution test is required. A Cobb 60 water-absorption result may be useful where moisture sensitivity is a concern, but the buyer must set the method, acceptance limit, and relevance to the package; no pass/fail threshold is supplied by the ISO source summarized here.
Likewise, treat dieline registration and crease allowances as converter-specific manufacturing controls. A hypothetical drawing review might flag a ±0.15 mm registration target for supplier feasibility review; this is an illustrative project target, not an ISO requirement or universal packaging tolerance. Confirm capability on the chosen press, board, and finishing route before it becomes a contractual limit. Structural prototyping is particularly valuable where a print panel crosses a crease, a coating changes fold behavior, or a tuck/lock feature is sensitive to board caliper.
Cost-down should preserve the approved function. Compare total landed cost rather than sheet price alone: board grade and yield, print coverage and finishing, tooling amortization, scrap risk, pack-out time, freight cube, and damage exposure all influence the commercial decision. For example, reducing blank size may improve board yield but can also reduce panel area or compromise compression geometry. Ask the supplier to show the revised dieline and the changed cost drivers; validate any structural trade-off with a prototype and the agreed test plan.
Practical conclusion: ISO 12647-1 is the print-process communication anchor; package performance requires a separate, explicit engineering specification. TadaPack can support custom structural packaging, dieline review, and prototyping so print intent and converting requirements are evaluated together. TadaPack’s online calculation tools are available at https://tadapack.com/tools; use them as planning aids, then confirm supplier and test-lab assumptions for the actual pack.
Procurement verification checklist
- ☐ Identify the print process, production substrate, artwork revision, and approved visual reference.
- ☐ Document the agreed print inspection method and acceptance criteria with the print supplier.
- ☐ Freeze and cross-reference the artwork file and converter’s dieline revision.
- ☐ Specify board construction and any applicable ECT grade separately from print requirements.
- ☐ Review caliper, crease, registration, coating, and adhesive requirements with the converter; label project tolerances as agreed supplier limits, not ISO limits.
- ☐ Select a distribution test protocol, such as ISTA 3A or ASTM D4169, only after confirming the relevant profile and acceptance criteria.
- ☐ Prototype material or geometry changes and reapprove both appearance and functional performance before production release.
Engineering decision figure
Figure takeaway: use ISO 12647-1 for the print-control scope, then define packaging tolerances and distribution validation independently.
Recommended Engineering Reading
[TOOLS] Featured Engineering & Calculation Tools
Explore 70+ Packaging Tools ➔Foil Stamping Area & Cost Calculator
Estimate hot foil stamping area, foil consumption, and die tooling costs.Imposition & Sheet Utilization Optimizer
Optimize parent sheet imposition layouts to minimize off-cut paper waste.
