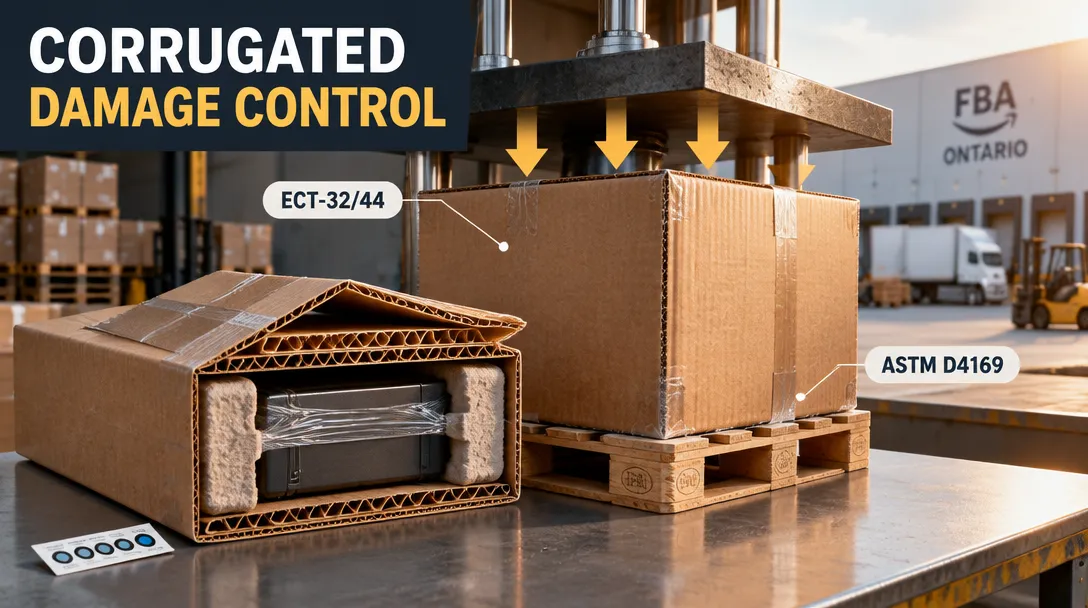
For shipments moving through Southern California fulfillment networks, a box that survives pallet storage can still fail after parcel handling, repeated conveyor transfers, vibration, and drops. The practical control is not simply to buy a higher ECT grade: specify the whole package, condition it for moisture, and verify it with the intended distribution environment and Amazon FBA dimensions.
Use the numbered process below to establish measurable design targets without treating them as universal pass/fail limits. Numerical values described as targets are starting points for engineering validation, not claimed test results or guarantees; no shipment-specific measurements were supplied.
1. Map the Inland Empire–FBA Ontario exposure before choosing board
Start with the real route and handling unit. Confirm the ship-from location, delivery appointment and receiving requirements, whether cartons travel as parcel shipments or on a pallet, and whether the product is conveyed or manually handled. Inland Empire fulfillment can involve multiple handoffs; model the expected parcel or unit-load distribution cycle rather than assuming a short truck journey is the only stress.
Record the packed gross mass, dimensions, product orientation, center of gravity, pallet pattern if applicable, and the locations where a carton can be struck or compressed. Amazon FBA dimensional and weight rules can affect fulfillment economics; confirm current program requirements for the relevant shipment before freezing dimensions. A smaller carton can reduce dimensional exposure only if the product has adequate clearance and protection.
For environmental inputs, ask carriers and fulfillment partners for route-specific dwell and storage conditions. High humidity can soften paper liners and reduce compression performance; dry inland storage does not eliminate moisture exposure acquired earlier in the journey. Cobb water absorptiveness is measured under TAPPI T441, but a Cobb result alone does not predict finished-box performance or prove resistance to every moisture mechanism.
- ☐ Confirm parcel versus palletized handling, shipment mass, dimensions, and orientation.
- ☐ Identify likely compression, vibration, drop, and moisture exposures with the logistics provider.
- ☐ Check current FBA carton limits, labeling, and dimensional/weight rules before release.
2. Set an ECT, flute, and moisture specification that fits the load
Choose corrugated board using box geometry, gross mass, stacking duration, humidity, and internal support—not ECT in isolation. ECT-32 and ECT-44 are useful comparison points for board edgewise crush resistance; specify the applicable test method, such as TAPPI T811, and require supplier documentation for the ordered construction. ECT is not box compression strength (BCT), and neither value by itself accounts for box dimensions, joints, openings, or package conditioning.
Consider E-flute for compact, well-supported packs where print and smaller profile matter; B-flute for a practical balance of cushioning and stacking support; C-flute where greater cushioning and panel stiffness are needed; and BC double-wall where load, stacking, or handling risk justifies the added material. These are selection directions, not fixed caliper guarantees: flute caliper varies by mill and construction, so set caliper from the approved board specification and verify incoming lots. Do not assume a named flute alone guarantees performance.
For heavier or less uniform loads, compare ECT-32 with ECT-44 in a finished-box compression and distribution test. Consider wet-strength or barrier treatments only after checking recyclability, adhesive compatibility, and the actual exposure. If a coating is used, specify PFAS-free chemistry where required by customer or market policy and substantiate claims. For EU-bound packaging, review Regulation (EU) 2025/40 on packaging and packaging waste (PPWR), including its application timetable and relevant requirements; do not describe a package as compliant based solely on a material label.
Q: Is ECT-44 automatically the safer choice than ECT-32 for FBA Ontario?
No—ECT-44 is not automatically safer. ECT rates edgewise board crush, while finished-carton failure also depends on box dimensions, seams, humidity, product support, and parcel impacts. Specify the lowest-cost construction that passes the agreed distribution test with the product packed, and escalate from ECT-32 to ECT-44 or a different flute only when testing identifies a need.
3. Engineer fit, cushioning, and closure as one protective system
Set product-to-carton clearance from the product’s fragility and the cushioning material’s working range. Avoid a universal clearance number: a rigid, low-fragility item and a brittle product need different designs. Specify insert position and allowable movement in the CAD drawing, then verify that the product cannot contact vulnerable carton panels during expected impacts. Molded-pulp components should be checked for fit, nesting, and dimensional variation against supplier capability; do not substitute nominal dimensions for a physical fit check.
Design the closure and converting geometry to resist flap opening and corner crush. Check that slot and score locations leave adequate panel support, that tape or adhesive is compatible with the board surface, and that sealing remains intact after conditioning. For die-cut work, use a drawing-controlled registration tolerance agreed with the converter; a proposed ±1 mm registration target can be a starting point for prototype review, not a universal industry standard. Confirm the converter can hold it on the actual design.
Use box compression calculations only as screening tools. McKee-type estimates can help compare alternatives, but actual BCT depends on board properties, box perimeter, aspect ratio, joint quality, and environmental conditioning. For stack loads, calculate the lowest-carton demand from the actual pallet pattern and stack height, then apply a documented safety factor that accounts for dwell, humidity, and load variability. Do not invent a universal derating factor for the Inland Empire; obtain the operating assumptions from the shipper and validate the package.
4. Build and test a corridor-representative package
Test production-representative cartons with the real product, inserts, closure, and labels. ASTM D4169 provides a distribution-cycle framework for evaluating shipping containers and systems; select the distribution cycle and assurance level to match the shipping mode and risk. Use the current applicable procedure and laboratory guidance rather than treating one vibration setting or one drop sequence as suitable for every FBA shipment. ASTM D642 can be used to measure compressive resistance of shipping containers, but compression testing does not replace distribution testing.
- Step 1 — Freeze the shipment definition. Record packed mass, outside dimensions, product orientation, handling mode, and expected stack. Tolerance: drawing dimensions and mass must remain within the approved product and carrier limits; do not release a design with an undefined shipment configuration.
- Step 2 — Approve the board and converting specification. State flute, wall construction, ECT target such as ECT-32 or ECT-44, test method, joint, and closure. Tolerance: accept board only within the supplier’s documented specification and agreed incoming inspection limits; no generic ECT tolerance is assumed here.
- Step 3 — Verify fit and conditioning. Pack production-intent samples and inspect insert position, movement, flap alignment, and closure. Tolerance: use drawing-defined clearance and converter registration limits; a proposed ±1 mm registration target requires converter confirmation before adoption.
- Step 4 — Validate distribution performance. Run an agreed ASTM D4169 distribution evaluation and inspect product, carton, seams, and labels afterward; use ASTM D642 when compression is a relevant failure mode. Tolerance: pass/fail criteria must be defined in advance for product damage, closure integrity, and carton function; do not claim a pass without recorded test evidence.
5. Check results, correct failure modes, and control procurement changes
Before approving a design, compare the test record with the pre-agreed acceptance criteria. Inspect for product damage, panel buckling, corner crush, popped flaps, seam separation, insert displacement, and label readability. Record carton dimensions and mass from representative production samples, and retain the approved drawing, board specification, closure instructions, and change-control requirements. Revalidate after a material, supplier, geometry, or pack-out change that could affect protection.
For moisture concerns, compare conditioned and exposed specimens using an agreed conditioning and test plan; ISO 186 specifies sampling for paper and board, while conditioning should follow the applicable test method and laboratory protocol. Do not apply a single humidity adjustment as a guaranteed strength correction. If compression loss or delamination is observed, investigate moisture history, liner bonding, board construction, and storage before adding board weight.
Common failures have distinct corrective paths. Flap popping points first to closure application, flap geometry, or carton overfill; verify the pack-out and sealing process before changing board grade. Corner crush or panel buckling points toward compression demand, unsupported spans, or poor pallet alignment; review stack load, box dimensions, and board construction. Adhesive separation calls for checks of adhesive coverage, surface condition, cure, and humidity exposure. In every case, change one controlled variable at a time and repeat the relevant test.
TadaPack can support custom structural packaging design and prototyping for shipment-specific fit and protection reviews. Use the online tools at https://tadapack.com/tools for preliminary calculations, then confirm assumptions with supplier specifications and physical testing. Calculator outputs are screening estimates, not certification.
Recommended Engineering Reading
[TOOLS] Featured Engineering & Calculation Tools
Explore 70+ Packaging Tools ➔CBM Volume & Freight Dim-Weight Calculator
Calculate cubic meters & dimensional weight to minimize freight costs and avoid FBA size tier penalties.Mailer Box Area & Dieline Size Calculator
Instant flat dieline dimensions, material consumption, and sheet nesting for custom D2C mailer boxes.
Frequently Asked Technical Questions (FAQ)
Should I use ECT-32 or ECT-44 for cartons shipped to FBA Ontario?
Which test protocol is relevant for reducing parcel damage on this corridor?
Does a higher ECT value guarantee better box compression?
How should moisture-related corrugated failures be investigated?
