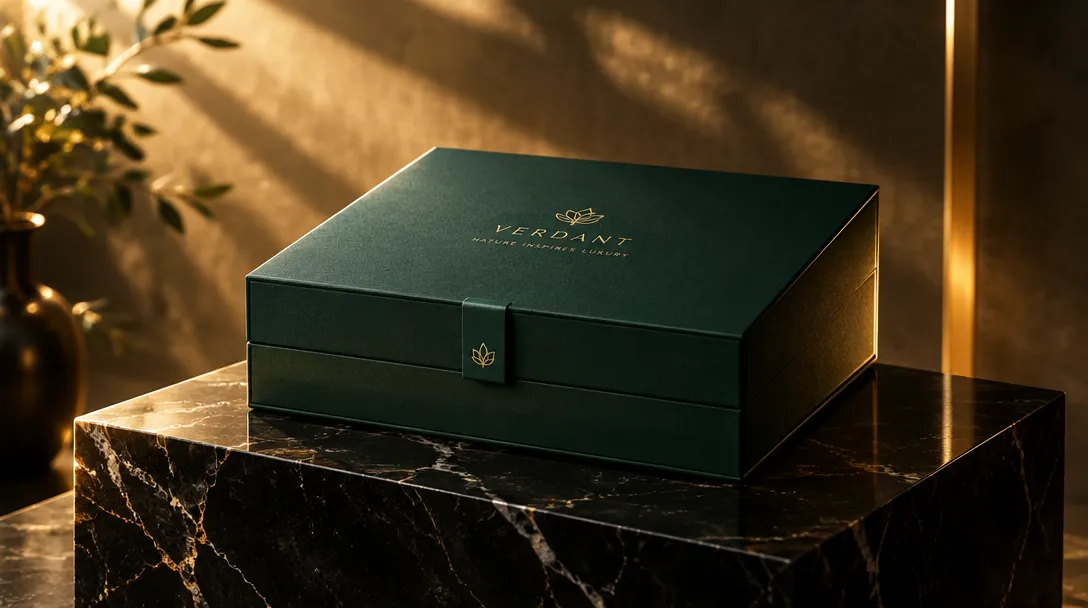
Wholesale magnetic closure (book-style/hinged lid) rigid boxes are engineered from 1.0-2.5mm laminated grayboard with embedded magnet pairs rated 800g-2,500g pull force, wrapped in 128-157gsm art paper or specialty stock. At wholesale volumes (500-2,000+ MOQ), landed unit cost is dominated by grayboard caliper, wrap decoration passes, and magnet insertion labor—so spec these three variables first and verify with ASTM D642 and ISTA 3A protocols before tooling release.
- Magnet pull force, not board thickness, is the primary quality lever: specify 800g-1,200g for lightweight contents (<300g) and 1,800g-2,500g for rigid multi-component kits to prevent lid sag and transit pop-open under ISTA 3A drop sequences.
- Grayboard caliper drives 40-60% of unit cost: moving from 1.5mm to 2.5mm board raises material cost roughly 55-70% in hypothetical worked examples, so right-size caliper to compressive load using ASTM D642 bench testing.
- MOQ is a decoration problem, not a printing problem: digital wrap printing supports 500-unit MOQs; hot foil stamping, soft-touch lamination, and embossing brass dies push practical MOQs to 1,000-2,000 units due to setup amortization.
- Ocean transit humidity is the #1 field-failure driver: grayboard with Cobb 60 water absorption above ~180 g/m² can warp and delaminate wrap seams across 30-day Pacific corridors—demand board moisture conditioning and stretch-wrap + desiccant containerization.
- 2026 EU PPWR (Regulation 2024/1991) recyclability requirements: magnet housings and non-paper closures must support fiber-recoverable design; document material declarations per FTC Green Guides (16 CFR Part 260) for US recyclability claims.

Wholesale Magnet Box Economics Have Shifted Toward Caliper and Closure Optimization
Procurement interest in magnetic closure rigid boxes has accelerated as DTC electronics, cosmetics, and premium spirits brands consolidate SKUs—but the wholesale buying decision in 2026 is fundamentally an engineering trade-off, not a print buy. Three variables dominate the bill of materials (BOM): grayboard caliper (typically 1.0mm, 1.5mm, 2.0mm, or 2.5mm laminated grayboard), wrap substrate (128-157gsm coated art paper, specialty textured stock, or cloth), and the magnet assembly (ferrite vs. neodymium pairs recessed into board channels with adhesive and kraft tape cover). In a hypothetical worked example for a 250×180×60mm book-style box, the board accounts for roughly 45-55% of ex-works unit cost, decoration 25-35%, and magnet insertion plus assembly the remainder.
Magnet specification deserves engineering rigor. Ferrite magnets are cheaper and corrosion-resistant but deliver lower pull force per volume; neodymium (NdFeB) magnets deliver 3-5× the pull force density, enabling slimmer housings. A common procurement error is overspecifying magnet strength to compensate for lid misalignment—correct root cause is dimensional tolerance on the board channel depth (target ±0.15mm), not magnet grade. Under-specification is worse: lid pop-open during ISTA 3A drop sequences (26 drops, per the sequence defined in the protocol) is the single most reported field complaint for magnet boxes carrying rigid contents.
Why MOQ, Tooling, and Decoration Passes Set the Real Floor Price
Wholesale pricing for magnetic closure boxes is setup-cost amortized. A rigid box line requires: grayboard die-cutting (setup die, reusable across orders), wrap printing plates or digital profile, lamination, foil dies if hot stamping (brass or magnesium dies, $80-250 typical tooling in hypothetical benchmarks), magnet channel routing, and hand or semi-automatic assembly. Digital print wraps eliminate plate costs and enable 500-unit MOQs with per-unit premiums of roughly 15-30% over litho-laminated wraps at equivalent volumes. Conventional offset litho lamination becomes cost-advantage near 1,500-2,000 units. Hot foil, embossing, and spot UV each add a setup line item and typically add 0.5-1.5 percentage points of scrap allowance—reputable manufacturers quote 3-8% overage scrap per run.
Compression and stack performance must be validated, not assumed. Rigid setup boxes are not corrugated and carry no ECT rating; their stacking behavior is characterized per ASTM D642 (compressive resistance of shipping containers) on the shipping carton system, not the rigid box alone. For e-commerce fulfillment, the outer shipper is typically an ECT-32 single-wall or ECT-44 double-wall corrugated case selected against the McKee-derived stacking requirement, with the magnet box as the interior cushioned unit tested under ISTA 3A General Simulation.
【💡 Packaging Engineer’s Quick Q&A】
Q: If the corrugated shipper passes ASTM D642 compression, why do magnet-box lids still arrive popped open after airfreight?
A: Direct answer—compression and drop are independent stress modes; D642 validates stacking, not shock. Mechanical reason—ISTA 3A drop sequences generate transient deceleration that momentarily overcomes magnet retention force if pull force margin is below ~2× the lid’s effective inertial load, especially at low temperatures where ferrite magnet flux density drops. Procurement recommendation—require a magnet pull-force spec sheet (grams per pair, measured with a pull gauge) and mandate ISTA 3A with the actual kit contents, not dummy weights, before approving the production PO.
Transit Risk, Recyclability Compliance, and the 2026 Regulatory Picture
Ocean freight remains the dominant failure environment. Container sweat across Pacific and Atlantic routes drives grayboard moisture pickup; because grayboard is unsized recycled fiber, panels can cup and wrap seams can ridge when equilibrium moisture content swings several points over a 30-day sailing. Specify board with controlled moisture conditioning, ship in stretch-wrapped pallets with desiccant, and for high-humidity corridors consider poly-lined master cartons. The EU PPWR (Regulation (EU) 2024/1991) is now reshaping rigid box design for European-bound wholesale programs: packaging must be designed for fiber recycling, with non-paper components (magnet housings, plastic cover tapes) minimized or separable. For US markets, recyclability claims must be substantiated per FTC Green Guides (16 CFR Part 260)—a box marketed as ‘recyclable’ with embedded magnets needs documented access to regional recycling capability or a qualified claim. Additionally, any barrier coatings on wraps must be PFAS-free to avoid emerging state-level restrictions on intentionally added PFAS in food-contact-adjacent and general packaging.
A second compliance vector is dimensional freight economics. Magnetic closure boxes are low-density for their volume; retail-ready rigid boxes shipped as master packs frequently trigger Amazon FBA dimensional weight penalties if the master carton exceeds cube-optimized dimensions. Structural engineers should co-design the magnet box and the master case together—nesting two flat-packed halves or shipping lid-and-base sets inverted reduces master carton height 15-25% in typical worked examples, directly cutting freight class cost.
Recommended Actions: A Four-Step Wholesale Sourcing SOP
Procurement directors should run the following verification sequence before releasing tooling and POs:
- Step 1 — Lock structural spec and tolerances: define grayboard caliper (±0.15mm), wrap gsm, internal dimensions with 0.5-1.0mm clearance per product, and magnet pull force per pair (800g-2,500g range by content weight); require a signed dimension drawing with GD&T on magnet channel positions.
- Step 2 — Run short-run prototyping: commission 3-10 fully decorated prototype units (digital wrap, hand-inserted magnets) to verify closure feel, wrap seam alignment at corners, and lid overtravel; iterate before committing brass foil dies or litho plates.
- Step 3 — Validate against transit protocols: test the magnet box inside the actual shipper per ISTA 3A drop and vibration sequences, and test the master case per ASTM D642 compression; document magnet retention after full sequence—no lid pop-open and no magnet debonding allowed.
- Step 4 — Verify compliance and landed cost: collect material declarations (PFAS-free coatings, PPWR fiber-recyclable design notes, FTC Green Guides substantiation), then model landed cost including tooling amortization, 3-8% scrap overage, and dimensional freight—TadaPack’s free packaging calculation tools (https://tadapack.com/tools) let you interactively verify unit cost and freight-dimension math before issuing the PO.
TadaPack supports each step with custom structural packaging engineering and short-run prototyping services, from grayboard caliper selection through magnet assembly specification, so wholesale buyers can de-risk tooling release with physical samples rather than CAD renders alone. Common failure modes to bake into supplier QC: grayboard warping (root cause: lamination moisture imbalance—corrective: enforce ISO 186 conditioning and inspect flatness at receiving), and wrap adhesive debonding at magnet channels under ocean humidity (root cause: adhesive creep at recessed tape bridges—corrective: specify higher-tack hot-melt and require kraft tape reinforcement over each magnet channel).
Recommended Engineering Reading
[TOOLS] Featured Engineering & Calculation Tools
Explore 70+ Packaging Tools ➔Box Compression (BCT) Calculator
Predict box compressive limit and stacking safety factors via McKee formula.Edge Crush Test (ECT) Calculator
Calculate linerboard ring crush and composite ECT ratings for optimal board specs.
